3D TPU Heat Transfer Label Vendor: How to Choose the Best for Your Apparel
2026-10-08
Choosing the right 3D TPU heat transfer label vendor can make or break your apparel's brand identity. While many suppliers promise durability, few deliver the crisp, dimensional finish that sets premium garments apart. That's where Victorygen heat transfer label stands out—but not all vendors are created equal. In this guide, we'll walk you through the key factors to evaluate, from material quality and adhesion to turnaround time and customization options, so you can avoid costly mistakes and partner with a vendor who truly understands your production needs.
Does the TPU Actually Stretch With Your Fabric, or Just Sit on Top?
When TPU is heat-bonded or laminated directly to the fabric, it doesn't just sit there like a sticker. The film gets pressed into the surface fibers and forms a bond that lets it move with the material — at least up to a point. On stretchy knits and woven fabrics with elastane, a thin TPU layer will usually follow the fabric's pull without cracking, because the film itself has a fair amount of elongation before it hits its limit.
That said, the stretch isn't infinite. If the TPU is applied too thick, or if the base fabric has a very high stretch percentage, you'll notice the TPU starts to fight back. It might hold the fabric back, create wrinkles, or peel at the edges once the bond weakens from repeated pulling. The trick is matching the TPU's elongation to the fabric's stretch.
So the short answer is: yes, it stretches with the fabric when it's properly bonded and not over-applied. But if you treat it like a rigid coating and expect it to follow every movement of a highly elastic material, it will eventually sit on top and start to separate.
The Sampling Stage Where Most Vendors Quietly Cut Corners
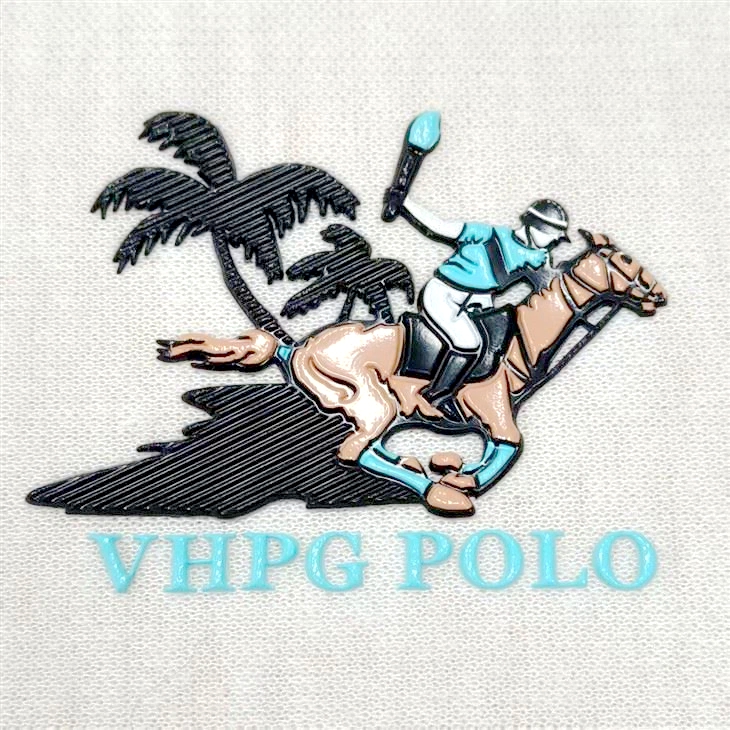
Ask five suppliers how they handle sampling and you’ll get five confident answers. Then ask to watch the process. What often happens next is revealing: a shared mold gets substituted, the resin grade shifts without a word, or the cure time shrinks just enough to hit a deadline. These changes rarely show up in the glossy sample that lands on your desk. They show up months later in yellowing, warping, or a sudden jump in scrap rates.
The easiest corner to cut is material sourcing. A vendor may run your first samples on the premium feedstock you approved, then quietly switch to a lower-cost blend for the second round. Unless you’re testing every batch with a spectroscope, you won’t catch it by touch. Color, gloss, and even weight can be tweaked with additives that mask the downgrade. By the time the production run fails, the original sample has long been filed away as “approved.”
Process discipline is another quiet casualty. Sampling under time pressure leads to shorter conditioning, skipped pre-drying, or molds pulled before full temperature stabilization. Each shortcut shaves hours or dollars, and each one nudges the part away from what you’ll actually receive in mass production. If your vendor can’t show you the sampling log with real timestamps and material lot numbers, assume the sample is a promise printed on warm paper.
Washing, Drying, Ironing—Testing Claims Before You Commit
Laundry labels promise a lot, but the real test happens at home. Before you buy a detergent that claims to brighten whites or a fabric softener that says it eliminates wrinkles, run a small side-by-side comparison. Wash one half of a stained cloth with your current product and the other with the new one. You will see fast whether the extra cost is justified. For drying, toss a mixed load in and check for shrinkage or stiffness after one cycle. Claims about low heat or gentle tumble mean little if your favorite shirt comes out tighter.
Ironing has its own set of half-truths. A spray starch might say it gives a crisp finish without flaking, but that depends on fabric type and your iron's steam output. Test it on an inside seam first, not on the front of a dress shirt. If you are thinking about switching to a steam generator iron, borrow one or buy from a store with a solid return policy. Run it over a wrinkled cotton napkin and a synthetic blouse to see if the heat and steam actually relax fibers instead of just dampening them.
Small tests like these take five minutes and save you from a shelf full of disappointing products. Keep notes on what works for your water hardness and machine type. What shines in a demo video often behaves differently with your routines, so let your own laundry room be the judge.
Why MOQs and Pricing Structures Affect Long-Term Design Freedom
Minimum order quantities quietly shape what a designer can actually commit to. When a factory demands 5,000 units before production starts, the pressure to pick safe, proven components becomes overwhelming. An experimental hinge or a custom-molded texture suddenly carries inventory risk that most teams cannot absorb. The result is a slow drift toward the middle of the road—designs that feel familiar because the economics punish curiosity.
Pricing structures often hide behind simple tier charts, but their real effect shows up months later. A steep discount at 10,000 units makes the cheaper material look smart on paper, yet that same material may limit future revisions. If the design later needs a softer durometer or a different finish, the tooling and supply agreements already lock the team into the original choice. The freedom to iterate shrinks precisely because the initial unit price felt too good to refuse.
Long-term design freedom depends on negotiating flexibility before the first purchase order. A modestly higher MOQ with the option to modify molds later can be worth far more than a lower price with rigid terms. Teams that treat MOQ and tier breaks as fixed constraints often discover too late that their product cannot evolve without starting over. The smart approach treats these numbers as variables to be challenged, not boundaries to accept silently.
Verifying Eco-Friendly TPU Ingredients Beneath the Green Label
A green label on TPU often leans on a single percentage—say, 30% bio-based—but that number means little without knowing how it was measured. Ask for the test method behind the claim. ASTM D6866 uses carbon-14 analysis to distinguish plant-derived carbon from fossil carbon, and it can flag blends where only a small fraction of the polyol is bio-sourced while the isocyanate remains entirely petrochemical. Request the full formulation breakdown, not a marketing sheet. If a supplier hesitates to share the percentage of renewable content in each monomer, that hesitation is itself a data point.
Certifications help, but only when they cover the specific grade you are buying. An ISCC PLUS certificate for a parent company does not automatically apply to a TPU pellet sold under a different trade name. Match the certificate number to the lot and check the mass balance approach—some certificates allow fossil and bio feedstocks to be mixed in the same reactor, which is legitimate but needs clear bookkeeping. Also watch for additives that quietly reintroduce petroleum: plasticizers, stabilizers, and flame retardants can easily make up 10–20% of the final compound. The green label should cover the whole formulation, not just the base resin.
What Happens When a Batch Goes Wrong—Vendor Accountability Signals
When a batch fails inspection or underperforms in the field, the first telling signs often surface in how the vendor communicates. A supplier that immediately shares batch records, retains samples, and walks through their in-process control data is signaling accountability. In contrast, vendors who deflect, delay providing the certificate of analysis, or suddenly change their story about raw material origins create a different kind of signal—one that suggests they may be covering up a process drift or an unapproved substitution.
Accountability signals also show up in the paper trail. Legitimate vendors can produce timestamped quality checkpoints, equipment maintenance logs, and deviation reports without being asked twice. If a batch goes wrong and you find yourself repeatedly chasing missing lot numbers, incomplete inspection sheets, or vague “we’ll look into it” responses, that’s a red flag. Real accountability means the vendor already has the data organized before the problem escalated, not after you start pressing.
Beyond documents, watch how the vendor treats the failed batch itself. Accountable suppliers will offer to quarantine remaining inventory, run root cause analysis with your team, and absorb reasonable costs for rework or disposal. Vendors who quietly reship the same lot to another buyer, refuse to share corrective action plans, or only respond when legal threats appear are broadcasting that their priority is offloading risk, not fixing the process. These behavioral patterns are the real vendor accountability signals—they tell you whether a bad batch is an isolated incident or a symptom of a deeper quality culture failure.
FAQ
Look beyond price. Check their production capacity, sample turnaround time, and whether they use virgin TPU material rather than recycled blends that may crack. Ask for references from brands in your apparel niche and request a pre-production sample to test wash durability.
Ask for wash test reports under conditions similar to your garments, like 40°C or 60°C with detergent. A trustworthy vendor will share data on adhesion strength, color fastness, and edge lift after at least 20 wash cycles. You can also run your own 50-wash test on a small batch.
Yes, in-house mold making usually means faster iteration and lower costs for design changes. It also avoids the communication lag that happens when a vendor outsources mold production. You'll get more consistent label dimensions and sharper details.
Many vendors start around 500 to 1,000 pieces per design, but some flexible suppliers offer low-volume options of 100 to 300 pieces for sampling or small capsule collections. Expect higher unit prices at lower quantities due to mold setup costs.
Request documentation for REACH, OEKO-TEX, or similar certifications. Ask if they use solvent-free adhesives and whether they have a waste recycling program for TPU offcuts. A genuinely eco-minded vendor will mention specific material suppliers and energy-saving production steps.
Some vendors have in-house designers who can adjust the height, gradient, and undercut of your 3D artwork to improve mold release and adhesion. Send them your vector file and ask for a 3D render before mold cutting. This reduces back-and-forth and prevents production surprises.
Watch out for vendors who quote extremely low prices without clarifying material thickness or adhesive type. Avoid those who can't provide a physical sample within a reasonable time. Also be cautious if they are vague about mold ownership, as some keep the mold and charge extra for future reorders.
It's critical. The adhesive must match your fabric type—cotton, polyester, nylon, or blends—and activate at a temperature that doesn't scorch the garment. Ask the vendor to recommend the right adhesive grade and provide a pressing parameter sheet for your heat press.
Conclusion
A label that refuses to stretch with your fabric will crack, pucker, or peel after a few wears. Ask a vendor to show you a swatch on an actual garment panel, not just a flat sample glued to paper. Pull it, twist it, and watch whether the TPU moves as one with the material or rides stiffly on top. During sampling, pay attention to how they handle small details—edge smoothness, underlayer adhesion, and whether they test your artwork at the exact size and thickness you intend to use. Many suppliers quietly swap to cheaper, thinner TPU after the first approval, so insist on a signed pre-production sample that locks in the exact film, gloss level, and durometer you approved.
Washing, drying, and ironing claims mean little until you test them yourself. Request a set of labels applied to your real fabric, then run them through at least five home laundry cycles, a hot dryer, and a steam iron on the recommended setting. Check for shrinkage, edge lift, color migration, and loss of embossed depth. On the commercial side, ask how the vendor structures MOQs and pricing—some hide setup charges or force you to order thousands of labels before you can tweak a design. A flexible partner will let you reorder smaller runs with minor artwork changes without punishing cost jumps. If they call a TPU film "eco-friendly," ask for the specific chemistry: Is it bio-based, recycled, or merely PVC-free? A trustworthy supplier will name the polymer blend and provide third-party test reports for restricted substances. Finally, watch how they react when a batch goes wrong. Do they blame the fabric, the printer, or the shipping? A vendor that owns the mistake, replaces the run fast, and adjusts their process is worth far more than one with a perfect green brochure and a stiff contract.
Contact Us
Contact Person: Wang Song Lin
Email: [email protected]
Tel/WhatsApp: +8613751282193
Website: https://www.heat-transferprinting.com/